


| Quantity: | |
|---|---|


RNE-SPHS-3000
SOLARAVEN
841912
The transition from fossil fuels to renewable thermal energy is essential for modern manufacturing facilities. Engineered for heavy-duty operational demands, this commercial solar boiler generate high temperature hot water more than 90℃ by solar thermal panels. By capturing abundant solar irradiation and converting it into usable industrial heat, facilities can successfully save electric bill of 60%~90%. The heavy-duty stainless steel tanks gleam under factory lighting, housing an advanced thermal core that operates with zero emissions and zero noise, making it highly suitable for house heating, drying, textile, food industry applications where consistent thermal energy is non-negotiable.
To accommodate facilities of varying sizes and production volumes, the solar boiler system capacity is range from 500liter to 100,000liter. Through a flexible modular design, the thermal storage and collection units integrate directly into existing factory pipe networks without disrupting ongoing daily operations. The thick, heavily insulated walls of the storage units retain intense heat for hours, ensuring that your production lines always have the necessary thermal resources on demand.
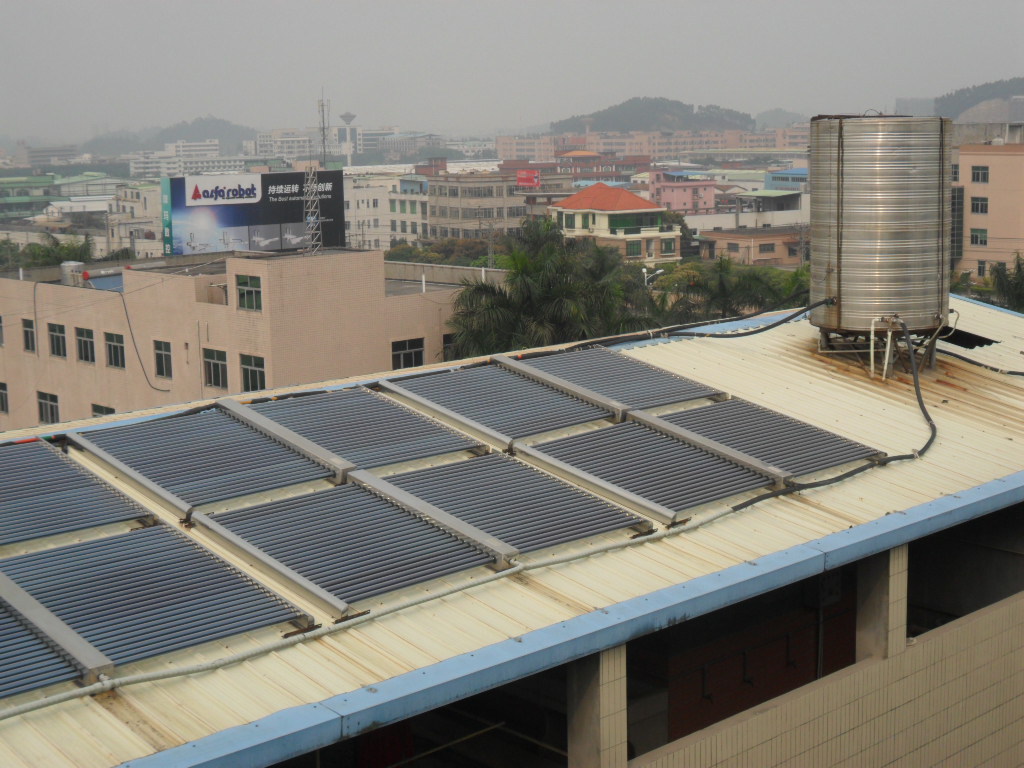
The exterior presents a clean, professional metallic finish that resists environmental wear, while the internal components are built to handle intense thermal stress day after day, securing your facility's energy independence.
The core advantages of industrial solar boiler lies in their significant energy-saving benefits, environmental characteristics, and long-term economic viability, making them particularly suitable for energy-intensive industries such as textiles and food processing. Every component is precision-engineered to maximize heat retention and operational safety.
In areas with good irradation conditiones, solar boiler can meet 60%-80% of industrial heating needs, resulting in an overall energy saving rate of 40%-50%. To ensure 24-hour uninterrupted production during rainy days or nighttime, the system features a sophisticated hybrid energy design. Facility managers can further reduce operating costs through peak-valley electricity pricing and multi-energy backup (such as combining with air source heat pumps or electric heating). An automated PLC control system manages this transition quietly and efficiently. Operators can monitor real-time temperature fluctuations and pressure metrics through a crisp digital interface, supported by multi-level safety valves to prevent over-temperature, over-pressure, and freezing conditions.
High efficiency and stability: Utilizing advanced solar vacuum tube and CPC reflector heat collection technology, the system concentrates solar radiation with extreme precision. The thermal efficiency reaches up to 105%, effectively generating steam at 80-300℃. You can feel the intense heat retained within the heavily insulated pipes, while the exterior remains completely cool to the touch, minimizing ambient thermal loss.
Constructed with industrial-grade stainless steel inner tanks and high-strength anti-corrosion brackets, the physical framework resists degradation even in humid or chemically active processing environments. This material choice guarantees water purity for sensitive applications. Long lifespan: The solar system has a lifespan of 25 years (compared to only 5-8 years for traditional boilers), resulting in exceptionally low maintenance costs. Based on real-world engineering data from energy-intensive sectors, the initial capital expenditure is rapidly offset by daily operational savings. Some case studies show that the investment cost can be recovered in just 4 years, providing decades of nearly free thermal energy thereafter.
Thermal energy is a foundational requirement across multiple manufacturing disciplines. This modular system provides targeted, high-capacity heating solutions for various demanding environments:
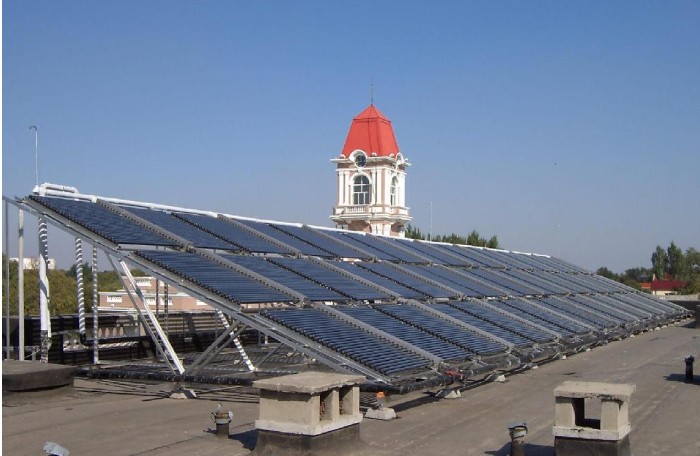
By adapting to these diverse applications, the system proves its versatility as a primary thermal generation asset.
Procuring heavy industrial equipment requires absolute confidence in safety, regulatory adherence, and long-term reliability. This solar thermal system is manufactured under strict quality control protocols, passing comprehensive ISO and CE certifications. Every pressurized component aligns with international pressure vessel manufacturing standards, ensuring complete compliance for complex facility upgrades worldwide.
Beyond the physical hardware, facility operators receive end-to-end technical support. The process begins with detailed thermal scheme design tailored to your specific site geography, existing pipe networks, and daily energy load. During deployment, expert engineers provide comprehensive on-site installation guidance to ensure proper integration. Furthermore, the system is backed by a 25-year lifecycle technical support program. Whether adjusting PLC parameters remotely or scheduling routine mechanical audits, the global maintenance network ensures your thermal generation remains uninterrupted, safe, and optimized for decades.


